|


 English
 Spanish
 French
 German
 Italian
 Chinese (Simplified)
 Japanese
 Korean
 Arabic
 Portuguese
 Call Me Free

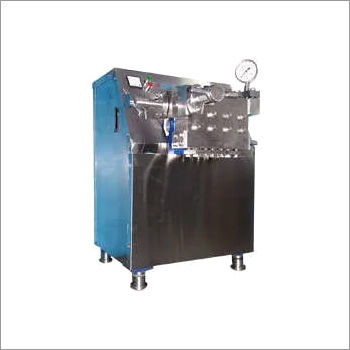
Industrial Milk Homogenizers
200000.0 INR/Set
Product Details:
- Product Type Milk Plant / Dairy Plant
- General Use Milk Process
- Material Stainless Steel
- Type Dairy Milk Plant Machinery, Dairy Production Machine, Milk Production Plant
- Capacity 500 LPH / 1000 LPH Ton/day
- Weight (kg) 6 Tons ( Approximately ) Metric Ton
- Computerized Yes
- Click to View more
X
Industrial Milk Homogenizers Price And Quantity
- 1 Set
- 200000.0 INR/Set
- 1100000.00 - 6000000.00 INR/Set
Industrial Milk Homogenizers Product Specifications
- Yes
- White / Green / Blue
- 420 Volt (v)
- Yes
- 40 Kilowatt (kW)
- PLC Control
- Milk Process
- CIP Cleaning System
- 500 LPH / 1000 LPH Ton/day
- Dairy Milk Plant Machinery, Dairy Production Machine, Milk Production Plant
- 40*30*20 Foot (ft)
- 6 Tons ( Approximately ) Metric Ton
- Milk Plant / Dairy Plant
- Stainless Steel
- Pasteurization
- 200 Bar
- Water Cooling
Industrial Milk Homogenizers Trade Information
- Coimbatore
- Letter of Credit (L/C), Cash in Advance (CID)
- 6 Set Per Year
- 2 Months
- Wooden Packing / Sea worth Wooden Pack
- Middle East, Asia, Africa
- All India
- ISO 9001 : 2015
Product Description
Experience instant savings and exceptional performance with our industrial milk homogenizers, boasting a rarefied blend of advanced technology and robust construction. Highly recommended for dairy processors, these uncommon machines feature PLC control for precision, a CIP cleaning system for convenience, water cooling, and automated pasteurization-ensuring smooth, safe milk processing. Select from 500 or 1000 LPH capacities, powered by an efficient 40 kW motor, all encased in durable, food-grade stainless steel. As a best-in-class manufacturer, exporter, and supplier across India, we provide trusted and timely service.
Versatile Applications & Noteworthy Features
Our industrial milk homogenizers are not limited to dairy production; they excel in processing other liquids such as juices, cream, and yogurts. Special features include computerized control, a high operating pressure of 200 bar, and customizable color options (white, green, blue). The machinery's large capacity and energy-efficient design are best suited for large-scale commercial use where uncommon reliability and consistent output are essential. These qualities make them the top select choice for specialized food and beverage plants.
Domestic Market Advantage & Streamlined Logistics
Primarily serving the vast Indian domestic market, our industrial milk homogenizers come with transparent payment terms, including advance and on-charge options for ease. Delivery time is carefully estimated based on order volume and requirements, ensuring machines are promptly dispatched to your location. Our clients benefit from reliable after-sales support and a streamlined supply chain, making purchase and installation processes seamless while minimizing any disruption to ongoing production lines.
Versatile Applications & Noteworthy Features
Our industrial milk homogenizers are not limited to dairy production; they excel in processing other liquids such as juices, cream, and yogurts. Special features include computerized control, a high operating pressure of 200 bar, and customizable color options (white, green, blue). The machinery's large capacity and energy-efficient design are best suited for large-scale commercial use where uncommon reliability and consistent output are essential. These qualities make them the top select choice for specialized food and beverage plants.
Domestic Market Advantage & Streamlined Logistics
Primarily serving the vast Indian domestic market, our industrial milk homogenizers come with transparent payment terms, including advance and on-charge options for ease. Delivery time is carefully estimated based on order volume and requirements, ensuring machines are promptly dispatched to your location. Our clients benefit from reliable after-sales support and a streamlined supply chain, making purchase and installation processes seamless while minimizing any disruption to ongoing production lines.
FAQ's of Industrial Milk Homogenizers:
Q: How does the PLC control system benefit milk homogenization?
A: The PLC control system offers precise automation and monitoring, ensuring consistent milk homogenization, reducing manual intervention, and enhancing overall process efficiency.Q: What are the main advantages of the CIP cleaning system?
A: The CIP (Clean-In-Place) cleaning system significantly simplifies equipment maintenance by allowing automated internal cleaning without disassembly, promoting hygiene and saving time.Q: When is the ideal time to integrate these homogenizers into a dairy plant?
A: Introducing these homogenizers during plant setup or major upgrades ensures that your facility achieves optimal process control, safety, and product quality from the outset.Q: Where are your milk homogenizers manufactured and supplied?
A: Our machines are manufactured in India and supplied nationwide, ensuring on-time delivery and localized support for industrial clients across the domestic market.Q: What uncommon features distinguish your milk homogenizers from others?
A: Our homogenizers offer high processing pressure up to 200 Bar, computerized controls, large-volume capability, custom color finishes, and advanced automatic operation, making them rare in both versatility and reliability.Q: How does usage of this machine impact dairy product quality?
A: Using our homogenizer ensures a uniform milk texture, enhanced shelf life, and improved product consistency-key quality benefits that set your dairy offerings apart in a competitive market.Tell us about your requirement

Price:
Quantity
Select Unit
- 50
- 100
- 200
- 250
- 500
- 1000+
Additional detail
Mobile number
Email

Other Products in 'Dairy Plant Homogenizers' category

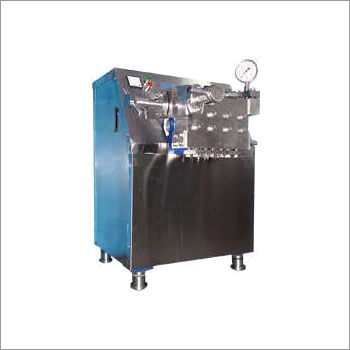

"All type of liquid and Semi-liquid Homogenizers are available."
Register As New Dealer
Contact Details
HARVEST HI-TECH EQUIPMENTS (INDIA) PVT LTD
GST : 33AACCH4145C1Z6
GST : 33AACCH4145C1Z6

Address
- No.16-B, Sarathy Nagar-1, Nandha Nagar Road, Singanallur,Coimbatore - 641005, Tamil Nadu, India
- Phone : 08045800611

 Send Inquiry

 Send Inquiry
 Send SMS
 |
HARVEST HI-TECH EQUIPMENTS (INDIA) PVT. LTD.
All Rights Reserved.(Terms of Use) Developed and Managed by Infocom Network Private Limited. |
